

Audible noise is evidence to investigate, but fault location depends on whether the sound tracks speed, torque or the machine structure. Changing measurement conditions can falsely imply a developing gear fault. Refer to the gearbox noise troubleshooting guidance. Include material throughput, motor frequency and ambient process sources. Analyze the associated rotating source before disassembly.
Start with a repeatable baseline
Examine mounting resonance
Escalate with structured evidence
Start with a repeatable baseline
A new sound should be compared with stable historical operation if records exist; distance, microphone position and nearby equipment affect how a recording sounds.
Changing measurement conditions can falsely imply a developing gear fault; record noise with constant observer position and actual operating rpm.

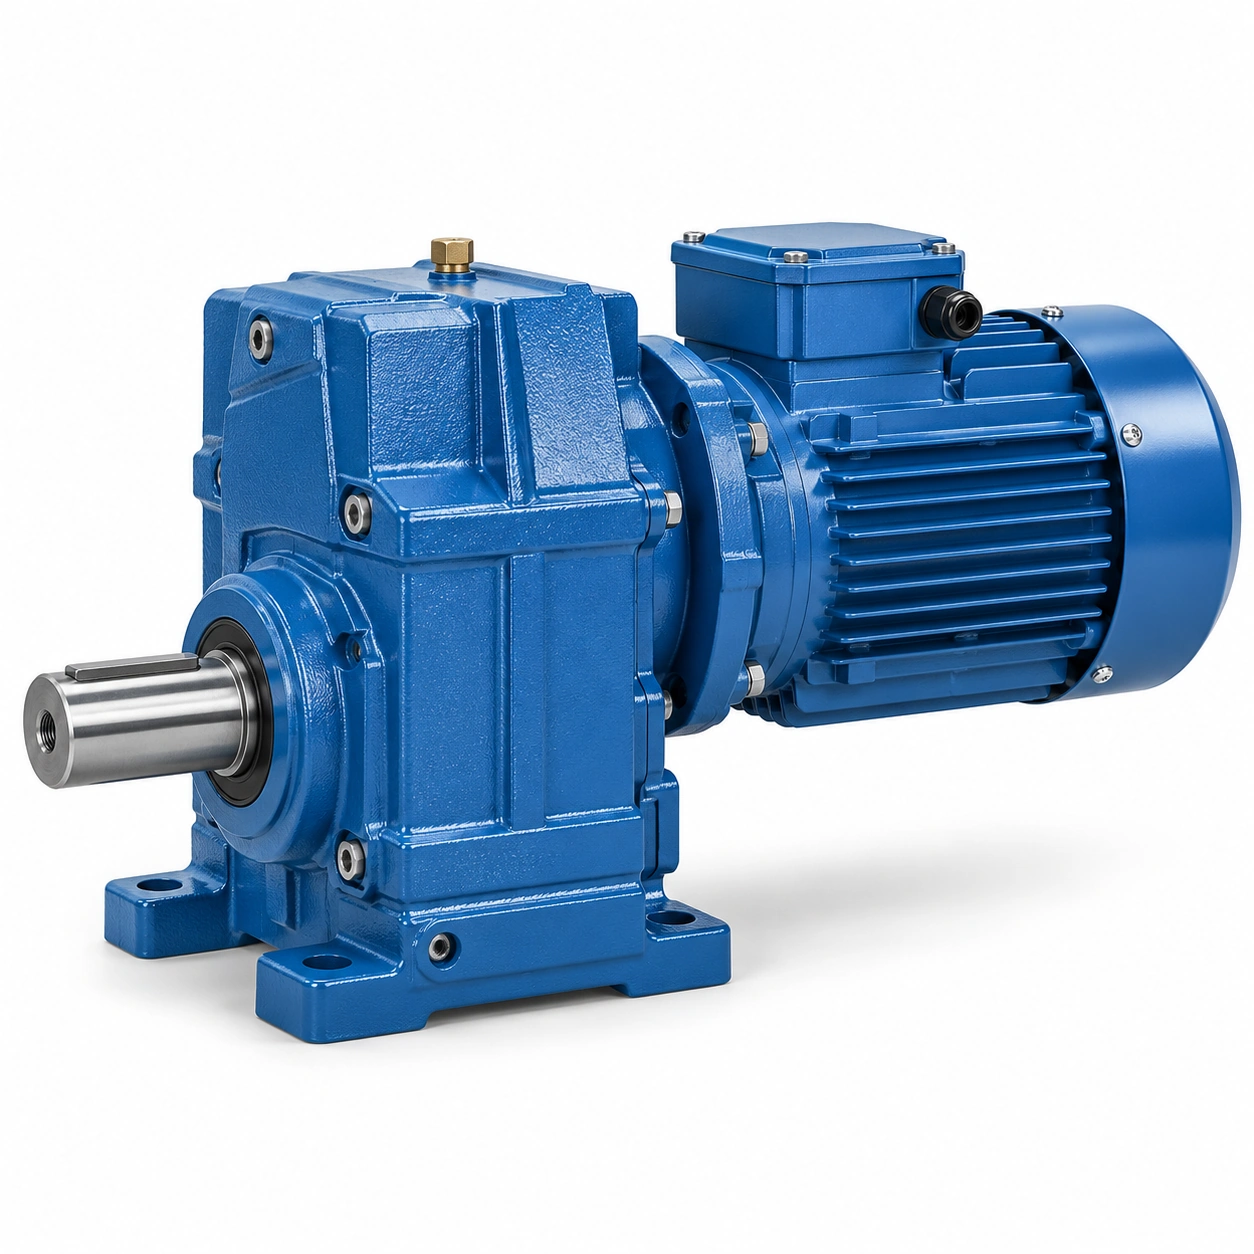
Include material throughput, motor frequency and ambient process sources; treat a consistent trend as stronger evidence than one isolated clip; a louder recording is not automatically a more damaged gearbox.
Separate speed-related components
Gear mesh and rotating elements generate components whose frequency moves with shaft speed; a tonal whine that rises with speed suggests a different pathway from an irregular impact once per product cycle.
Sound level alone cannot identify a damaged tooth or bearing; observe the same machine across safe controlled speed settings.

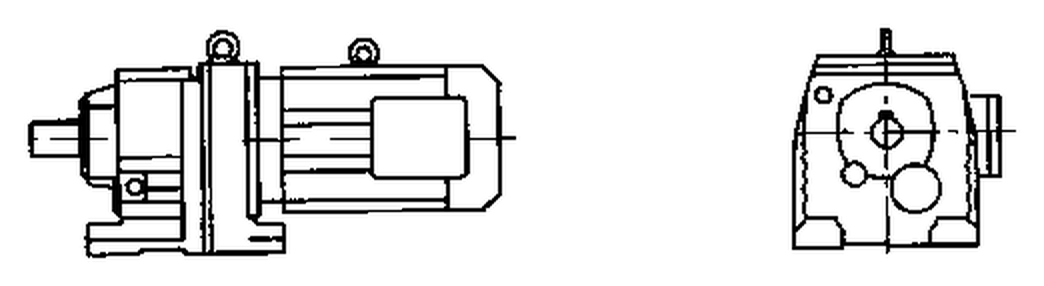
Log input and output rpm as well as the frequency change if instrumentation is available; analyze the associated rotating source before disassembly; changing speed can also excite an external structural resonance.
Compare loaded and unloaded sound
Gearing may sound different when tooth forces and bearing reactions increase under load; a conveyor at empty belt speed differs from one under a loaded start.
A quiet no-load run can hide defects that appear at production torque; observe safely under no-load, partial and normal loaded conditions.

Keep current and load estimates next to recordings of each state; use the load dependence to prioritize inspection targets; an unloaded test is not sufficient proof of tooth condition.
Exclude motor and fan sources
The gearmotor contains more than the reduction train and several components make sound; a motor cooling fan striking a guard can mimic an internal gearbox rattle.
Mistaking a fan or coupling source for a gearbox problem creates unnecessary repair cost; inspect accessible motor fan cover, coupling guard and adjacent components under isolation.
Use approved non-invasive tests to separate motor and reduction sources; confirm component identity before planning a gearbox teardown; removing safety guards while rotating equipment operates is not an acceptable diagnostic shortcut.
Examine mounting resonance
Thin panels and loosened structural mounts can amplify modest internal excitation; a machine sidewall may resonate in one rpm band and go quiet above it.
Amplified housing sound may not correspond to higher gear tooth stress; check foundation contact, foot bolts and guard attachment after safe isolation.

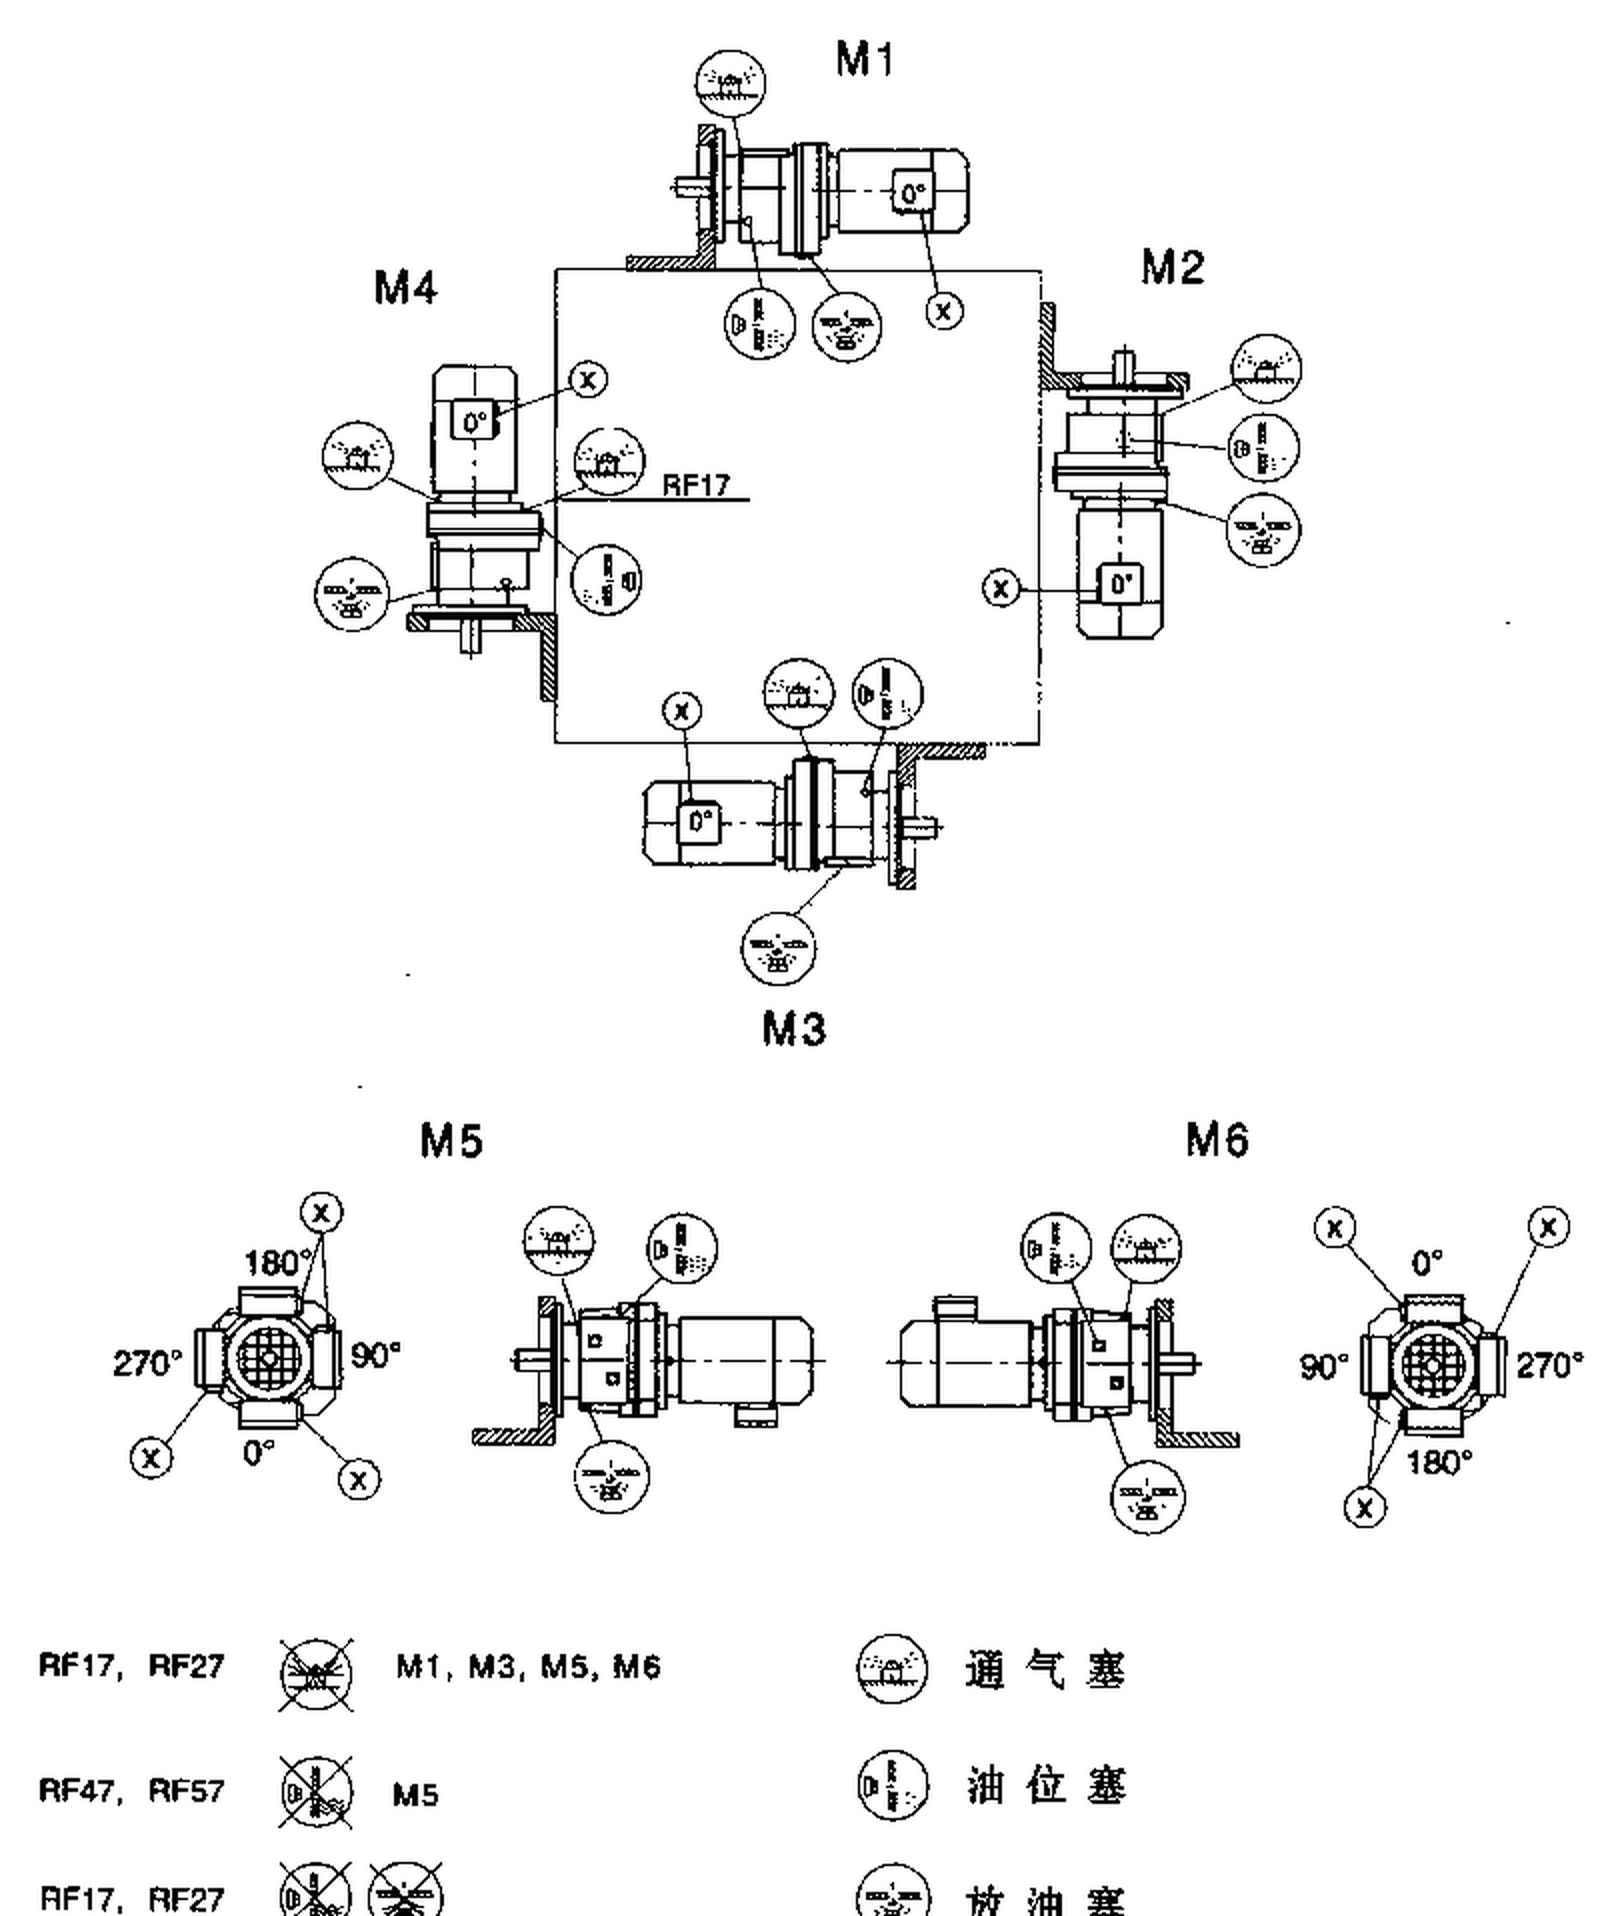
Compare frame vibration with housing vibration at equivalent speed and load; correct proven external looseness before claiming an internal fault; a flexible mount can turn small excitation into a major acoustic complaint.
A machine sidewall may resonate in one rpm band and go quiet above it. Amplified housing sound may not correspond to higher gear tooth stress. Examine the gearbox noise troubleshooting layout example. Compare frame vibration with housing vibration at equivalent speed and load. Correct proven external looseness before claiming an internal fault.
Relate sound to oil condition
Low oil level, foam or contamination may change both friction and noise; a new whining sound with an abnormal temperature trend merits prompt controlled inspection.
Adding oil without finding the correct fill point may make the problem worse; read the mounting-specific level procedure and inspect external leaks.

Record recent lubricant service, oil appearance and stable operating temperature; use manufacturer diagnostic guidance to determine safe continued operation; discolored oil alone does not identify a specific damaged gear element.
Collect time-of-onset clues
A noise that started after a coupling replacement has a different evidence trail from gradual wear; maintenance events, process changes and jam incidents create useful causal hypotheses.
Ignoring the change history can waste time looking at normal gear noise; build a chronology of the first complaint and nearby mechanical work.
Ask operators which recipe, shift and machine state make the sound strongest; prioritize checks supported by both symptom and event history; a plausible story is not proof until the mechanical evidence agrees.
Escalate with structured evidence
Specialist diagnosis benefits from synchronized audio, vibration and operating data; providing only a vague complaint often generates a generic recommendation to replace parts.
Unverified remote diagnosis can miss a safety-critical developing defect; supply plate photographs, rpm, load, sound location and recent work history.
Compare observation with maker guidance and qualified vibration analysis; determine a controlled shutdown or inspection plan based on evidence and risk; unsafe operation should not continue while waiting for a convenient repair window.
Illustrative engineering scenario: A production gearbox with a newly reported acoustic change
An operator reports that a gearbox has started to whine during a high-throughput packaging shift. The noise is not obvious during early-morning checks when the line is empty. Maintenance does not immediately conclude that the gears are worn. Instead, the team records three controlled observations: the machine idling at normal motor frequency, the conveyor carrying a partial load and production running at a representative full load. Each record includes output rpm, approximate throughput, motor current and a short audio sample taken from the same safe location. The sound changes mainly with torque, not just speed. That is a useful clue, but it does not identify a particular damaged component.
A recent maintenance entry shows that the driven coupling was removed three days earlier. The team isolates the equipment, inspects the coupling hub seating and verifies alignment. The protective guard is also checked for loose attachment because its thin metal panel may amplify a normal mesh frequency. Lubricant level is verified for the installed mounting position without opening or removing anything while the drive is rotating. If the housing also shows unusual temperature or a rapidly deteriorating vibration trend, continued operation should be governed by the plant risk process rather than by a casual judgment that the sound is probably normal.
For a useful manufacturer enquiry, attach the complete gearmotor identification, sound chronology, process conditions and findings from safe external inspection. Include both circumstances when the noise occurs and when it disappears. The service specialist may recommend vibration analysis, oil inspection or a planned teardown. Conversely, a loose guard or misaligned coupling may be corrected without opening the gearbox. The key distinction is between a working hypothesis based on controlled observations and a verified fault supported by multiple evidence sources.
The investigation team should also record how long the abnormal sound has persisted. A short change observed only during one product jam is different from a tonal noise that increases across many shifts. If a controlled inspection points to the coupling or frame, document the confirmed defect and repeat the same measurement after correction. The goal is to keep observed evidence separate from the conclusion so that a later technician can evaluate the reasoning.
Five-stage review for a production gearbox with a newly reported acoustic change
-
Start with a repeatable baselineRecord noise with constant observer position and actual operating rpm. Treat a consistent trend as stronger evidence than one isolated clip.
-
Separate speed-related componentsLog input and output rpm as well as the frequency change if instrumentation is available. Changing speed can also excite an external structural resonance.
-
Exclude motor and fan sourcesInspect accessible motor fan cover, coupling guard and adjacent components under isolation. Confirm component identity before planning a gearbox teardown.
-
Relate sound to oil conditionRecord recent lubricant service, oil appearance and stable operating temperature. Discolored oil alone does not identify a specific damaged gear element.
-
Escalate with structured evidenceSupply plate photographs, rpm, load, sound location and recent work history. Determine a controlled shutdown or inspection plan based on evidence and risk.
Engineering comparison matrix: helical gearbox abnormal noise troubleshooting
| Engineering question | Evidence to collect | Review decision |
|---|---|---|
| Start with a repeatable baseline | Include material throughput, motor frequency and ambient process sources. | Treat a consistent trend as stronger evidence than one isolated clip. |
| Separate speed-related components | Log input and output rpm as well as the frequency change if instrumentation is available. | Analyze the associated rotating source before disassembly. |
| Compare loaded and unloaded sound | Keep current and load estimates next to recordings of each state. | Use the load dependence to prioritize inspection targets. |
| Exclude motor and fan sources | Use approved non-invasive tests to separate motor and reduction sources. | Confirm component identity before planning a gearbox teardown. |
| Examine mounting resonance | Compare frame vibration with housing vibration at equivalent speed and load. | Correct proven external looseness before claiming an internal fault. |
| Relate sound to oil condition | Record recent lubricant service, oil appearance and stable operating temperature. | Use manufacturer diagnostic guidance to determine safe continued operation. |
Frequently Asked Questions
Does a whining helical gearbox always have worn gears?
What should accompany a gearbox noise recording?
Why does noise sometimes appear only when loaded?
When should operation be stopped rather than monitored?
What makes a final review credible for a production gearbox with a newly reported acoustic change?
Maintenance events, process changes and jam incidents create useful causal hypotheses. When comparing actual mounting geometry, use the gearbox noise troubleshooting configuration options. Ask operators which recipe, shift and machine state make the sound strongest.
Supply plate photographs, rpm, load, sound location and recent work history. For an engineering quotation that records the open conditions, contact the technical team about gearbox noise troubleshooting. Determine a controlled shutdown or inspection plan based on evidence and risk.
Engineering sources for Helical Gearbox Noise Diagnosis by Speed and Load
For the helical gearbox noise diagnosis by speed and load workflow, consult these reference documents alongside the actual model installation manual:
- Helical Gearbox Noise Diagnosis by Speed and Load: SKF Evolution, Parallel condition monitoring (analysis).
- Helical Gearbox Noise Diagnosis by Speed and Load: SKF, Bearing App documentation (interface review).
- Helical Gearbox Noise Diagnosis by Speed and Load: SEW-EURODRIVE, Lubricant tables (acceptance checks).