


SWP-C Short Non-Flexible Universal Joint Couplings: engineering overview
For SWP-C Short Non-Flexible Universal Joint Couplings, the most useful way to read the product data is to begin with the drive requirement and then confirm geometry. The description below therefore separates operating principle, configuration details, selection checks, installation and maintenance before presenting the source specification data.
This design transmits rotary power through a cross-and-bearing joint arrangement, so the connected shafts can run at an angle instead of requiring a perfectly straight centerline. In heavy drivetrains the joint is selected not only for torque, but also for operating angle, rotational speed, flange geometry, shaft spacing and the way axial movement is handled.
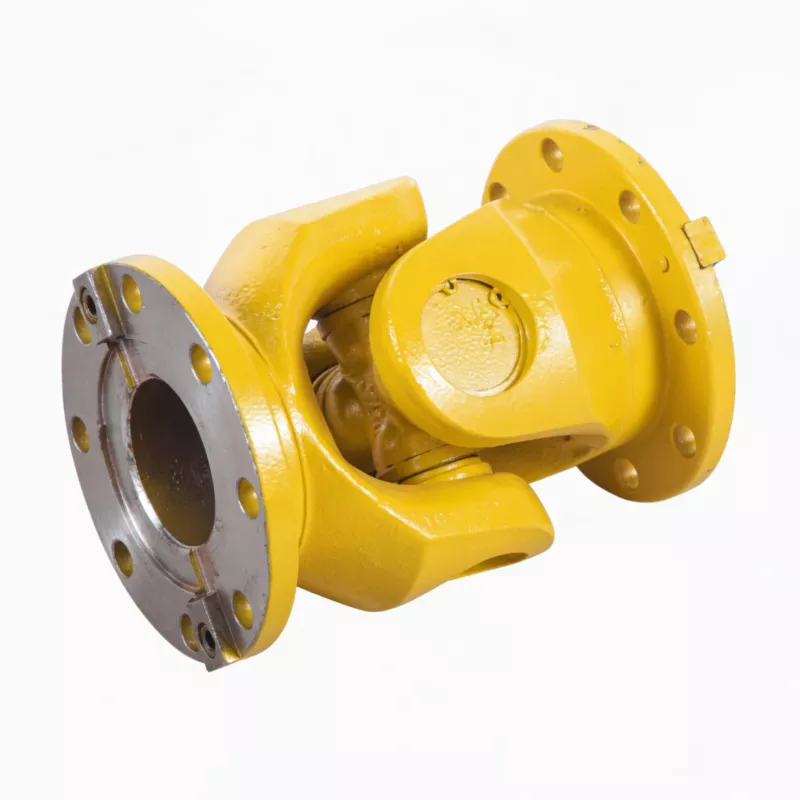
Key Features & Design Characteristics
Angular articulation
Cross-joint geometry accommodates shaft angles that cannot be handled by a rigid connection.
Heavy-duty torque path
The joint arrangement is intended for industrial drivetrains where torque transfer and mechanical robustness are primary selection factors.
Installation flexibility
Model geometry is checked against flange size, shaft spacing, working angle and available installation envelope.
Serviceable construction
Inspection planning can focus on the cross-bearing area, fasteners, lubrication condition and shaft movement where applicable.
How this version is configured
A universal-joint assembly should be treated as part of the complete driveline rather than as an isolated component. Joint angle affects velocity fluctuation, bearing load and service life, while the shaft span influences critical-speed behavior. For two-joint layouts, correct yoke phasing and a sensible distribution of angular offset are important for smoother rotation.
- The short-body arrangement reduces the required shaft-to-shaft installation length.
- This version uses a fixed-length shaft section; it does not provide telescopic axial travel.
Selection sequence for a real machine
Start with transmitted torque and the expected peak or shock load, then verify allowable speed for the chosen size. Check flange pilot dimensions, bolt pattern, bore or mating-shaft details, minimum operating length and any required telescopic stroke. The actual working angle should remain inside the value listed for the selected model, with allowance for installation tolerances and machine movement.
- Define continuous torque, starting torque and any short-duration peak load instead of selecting from motor power alone.
- Confirm rotational speed and check whether balance, centrifugal loading or critical-speed limits affect the chosen size.
- Match every shaft interface: bore diameter, key or locking method, hub length, flange pilot, bolt pattern and available assembly clearance.
- Review angular, axial and parallel displacement separately. A coupling that tolerates one form of movement may have a much lower limit for another.
- Check the surrounding equipment for guards, brakes, bearings, seals and maintenance access before freezing the final outside diameter and overall length.
- Use the exact model matrix for the final dimensional decision; do not interpolate a bore, torque or speed value that is not listed.
Technical Specifications & Dimensions
Use the tables below as the dimensional and model reference. Confirm bore, shaft fit, speed, torque and installation envelope before final selection.

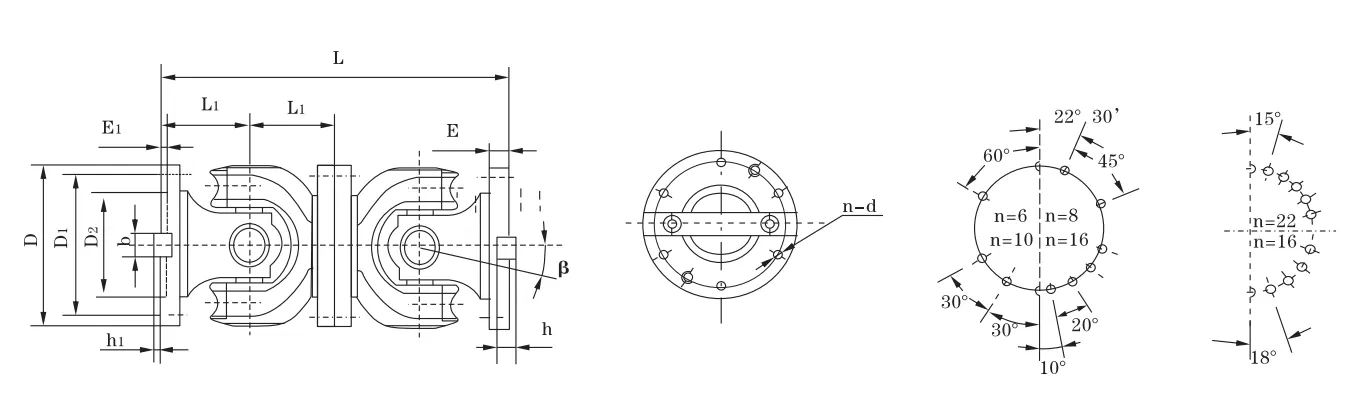
| Type | D (mm) | Tn (kN·m) | Tf (kN·m) | β | Lmin (mm) | D1 js11 | D2 H7 | E | E1 | b×h | h1 | L1 | n–d | I Lmin (kg·m²) | G Lmin (kg) |
|---|---|---|---|---|---|---|---|---|---|---|---|---|---|---|---|
| SWP160C | 160 | 16 | 8 | ≤10 | 340 | 140 | 95 | 15 | 4 | 20×12 | 6 | 85 | 6–13 | 0.11 | 31 |
| SWP180C | 180 | 20 | 10 | ≤10 | 380 | 155 | 105 | 15 | 4 | 24×14 | 7 | 95 | 6–15 | 0.17 | 42 |
| SWP200C | 200 | 31.5 | 16 | ≤10 | 440 | 175 | 125 | 17 | 5 | 28×16 | 8 | 110 | 8–15 | 0.29 | 59 |
| SWP225C | 225 | 40 | 20 | ≤10 | 520 | 196 | 135 | 20 | 5 | 32×18 | 9 | 130 | 8–17 | 0.51 | 80 |
| SWP250C | 250 | 63 | 31.5 | ≤10 | 540 | 218 | 150 | 25 | 5 | 40×25 | 12.5 | 135 | 8–19 | 0.93 | 119 |
| SWP285C | 285 | 90 | 45 | ≤10 | 600 | 245 | 170 | 27 | 7 | 40×30 | 15 | 150 | 8–21 | 1.88 | 179 |
| SWP315C | 315 | 140 | 63 | ≤10 | 680 | 280 | 185 | 32 | 7 | 40×30 | 15 | 170 | 10–23 | 2.88 | 232 |
| SWP350C | 350 | 180 | 90 | ≤10 | 740 | 310 | 210 | 35 | 8 | 50×32 | 16 | 185 | 10–23 | 4.59 | 300 |
| SWP390C | 390 | 250 | 112 | ≤10 | 820 | 345 | 235 | 40 | 8 | 70×36 | 18 | 205 | 10–25 | 8.64 | 432 |
| SWP430C | 430 | 355 | 160 | ≤10 | 940 | 385 | 255 | 42 | 10 | 80×40 | 20 | 235 | 16–28 | 17.41 | 688 |
| SWP480C | 480 | 450 | 224 | ≤10 | 1060 | 425 | 275 | 47 | 12 | 90×45 | 22.5 | 265 | 16–31 | 28.25 | 904 |
| SWP550C | 550 | 710 | 315 | ≤10 | 1160 | 492 | 320 | 50 | 12 | 100×45 | 22.5 | 290 | 16–31 | 49.49 | 1309 |
| SWP600C | 600 | 1000 | 500 | ≤10 | 1440 | 544 | 380 | 55 | 15 | 90×55 | 27.5 | 360 | 22–34 | 87.17 | 1377 |
| SWP640C | 640 | 1250 | 630 | ≤10 | 1540 | 575 | 385 | 60 | 15 | 100×60 | 30 | 385 | 18–38 | 152.76 | 2635 |
| Decision Factor | Choose SWP-C | Choose SWP-B or SWP-A Instead |
|---|---|---|
| Axial shaft movement in service | None — fixed positions | Any thermal growth, mechanical float, or sliding |
| Installation length priority | Shortest possible envelope | Length is flexible / standard |
| Lubrication access difficulty | Prefer fewer grease points | Grease access not a constraint |
| Rotational inertia sensitivity | Drive inertia must be minimised | Drive sizing allows higher inertia |
| Angular offset present | Yes (up to ≤10°) — SWP-C still compensates | Yes — both SWP-C and SWP-B compensate equally |
Standards and designation references found in the source data
Where a standard or designation is shown below, treat it as a reference tied to the original product data and verify the applicable revision when placing an order.

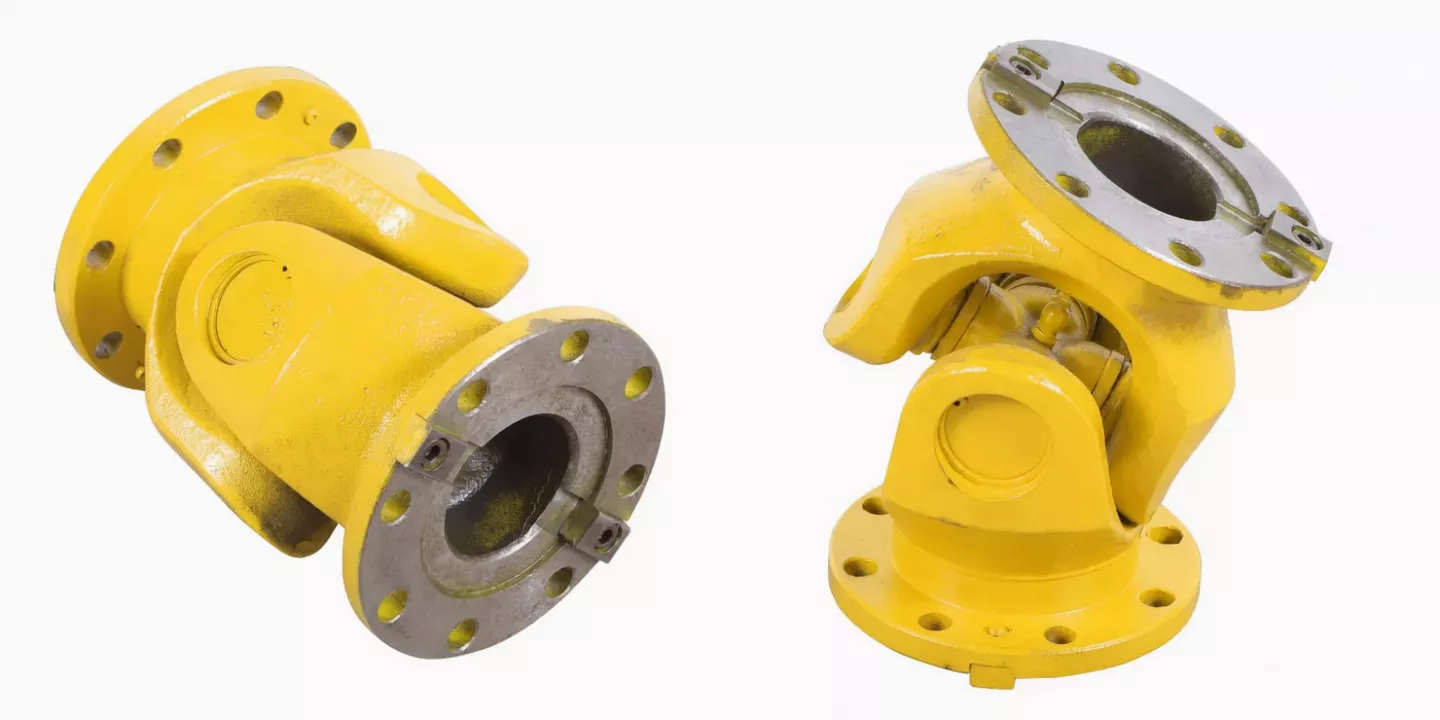
Shaft fit, alignment and assembly checks
Before assembly, confirm flange faces are clean, mating pilots seat fully and fasteners can be tightened evenly. Keep yokes in the intended phase relationship. On telescopic versions, set the slip section near the designed working position instead of installing it at either travel limit. Rotate the driveline by hand after installation to confirm there is no mechanical interference through the expected angle range.
Measure the actual shaft diameters and keyways before machining or confirming a finished bore. A drawing should identify shaft tolerances, key dimensions, required hub position and any shoulder, locknut or axial-retention feature. Alignment readings should be taken after the machine is in its normal installed condition because base distortion, pipe strain, belt pull or thermal growth can move the shaft centers after an initial bench alignment.
After assembly, turn the drive through at least one full revolution by hand where practical. Check for interference with guards, brake hardware and adjacent structures, then verify fastener security. On equipment that changes temperature significantly between start-up and steady operation, compare cold and hot alignment expectations before setting final offsets.

Operating behavior and service planning
Inspection should focus on cross-bearing condition, looseness at flange bolts, abnormal heat, seal damage and play in any sliding section. Where the joint uses grease lubrication, service intervals should reflect speed, duty cycle, contamination and temperature rather than a single calendar interval. A sudden increase in vibration or backlash is a reason to inspect the joint before continued heavy operation.
A coupling should not be used as a permanent correction for poor machine alignment. If vibration, temperature or noise changes after commissioning, compare the current condition with the initial baseline. Check connected bearings and shafts at the same time, because many coupling symptoms originate from looseness, soft foot, imbalance or movement elsewhere in the drivetrain.
For planned maintenance, record the installed model, actual bore sizes, fastener details, lubricant or flexible-element grade where applicable, and the measured alignment at return to service. That information makes later inspection more useful and helps distinguish normal wear from a change in machine condition.
Information to include with an RFQ or drawing review
- Required model or the closest model already identified from the specification data.
- Driving and driven shaft diameters, tolerances, keyways and available engagement length.
- Continuous torque, peak torque, starts per hour and whether the drive reverses.
- Normal and maximum rotational speed.
- Expected angular, axial and parallel movement during operation.
- Required overall length, shaft separation, flange or brake dimensions and surrounding clearance.
- Operating temperature, contamination, washdown, corrosion or other environmental conditions.
- Quantity, drawing revision and any material, coating, balance or inspection requirement.
Frequently asked engineering questions
Can I select this coupling only from the motor power?
No. Motor power is only a starting point. The selection should use actual torque, service factor, peak load, speed and the driven-machine characteristics.
Which dimension should be confirmed before ordering?
Confirm the shaft interface first, then the overall installation envelope. Bore, key or locking method, hub length, pilot or flange details and available removal clearance all affect whether a listed model will fit.
How much misalignment should be allowed in normal service?
Use the model-specific limit as a maximum capability, not as the target installation condition. Better initial alignment usually reduces cyclic load, heat and wear in both the coupling and connected bearings.
What information is needed for a custom bore or connection?
Provide a dimensioned shaft drawing or at minimum the shaft diameter and tolerance, keyway, engagement length, shoulder or axial-retention details and required hub position.
Should the coupling be inspected after commissioning?
Yes. A short follow-up inspection after the machine has run under real load can reveal fastener settlement, lubricant leakage, unexpected movement or alignment change before these develop into a larger problem.
How should I use the specification blocks on this page?
Treat the listed values as the model reference. Select a candidate from torque and speed, then verify every geometric field that affects your installation before issuing the final order drawing.
Applications
Rolling & process machinery
Suitable for drivetrains where connected shafts operate with angular offset or changing alignment.
Conveyors & material handling
Used where a robust rotating connection is required between separated drive components.
Lifting & handling equipment
Applicable to machinery with cyclic duty where shaft geometry and peak torque must be verified carefully.
Heavy industrial drives
Considered for equipment where installation space, working angle and service access are part of coupling selection.
Typical uses include rolling and processing machinery, mining equipment, conveyors, heavy industrial lines, lifting equipment and other drives where shafts are offset or move relative to one another. The final model should always be matched to the machine geometry and duty cycle rather than chosen from torque alone.
The same coupling family can behave very differently in a smooth continuous drive and in a reversing, impact-loaded or frequently started drive. For that reason, application name alone is not enough for selection. Supply the operating torque, peak load, speed, shaft dimensions, expected movement, ambient conditions and required service access so the configuration can be checked against the complete duty.